
How Plastiblends Brings Colour Masterbatches to Life
Understanding Colour Masterbatches and Their Importance
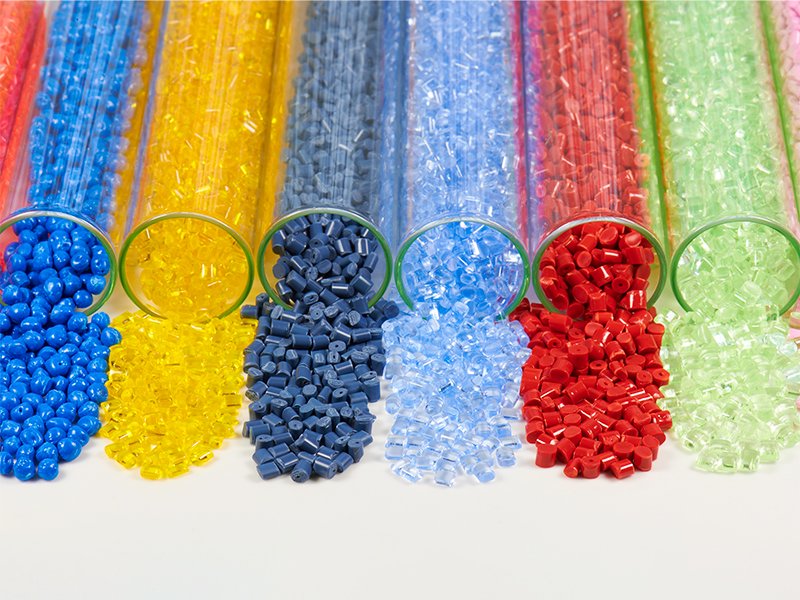
Colour masterbatches are concentrated mixtures of pigments or dyes encapsulated in a carrier resin, used to colour raw polymers during the plastic manufacturing process. These masterbatches are added in small, measured quantities to uncoloured plastic to impart vibrant, consistent and long-lasting colour.
Compared to traditional methods like powder pigments, they offer better dispersion, reduced dust, improved processing cleanliness and precise colour control.
At Plastiblends, Colour Masterbatches are not just one of our core product lines; they are the very essence of how we bring efficiency to the world of plastics. Our journey as a Masterbatches manufacturer is built on innovation, experience and consistency.
Colour Masterbatches Designed for Precision and Performance.
Our Colour Masterbatches are developed and designed to perform with exceptional quality and reliability. Whether our customers are in packaging, automotive, agriculture, electronics or any other sector, we ensure that the shades they choose are perfectly matched, thoroughly tested and backed by global standards.
Over 2,500 Colour Shades and Customised Formulations.
We bring to life over 2,500 existing colour shades, and our in-house colour matching labs work closely with clients to develop formulations that align with their unique requirements.
Our aim in this industry is simple but powerful: “Precision in every pellet.” This philosophy drives every aspect of our formulation and production process.
Advanced Pigment Dispersion and Colour Consistency.
Our team of colour technologists and engineers uses advanced equipment and pigment dispersion technology to achieve superior colour consistency, high opacity, excellent UV stability and resistance to weathering.
This ensures that colour does not simply enhance a product's appearance but also contributes to its longevity, protection from external elements and ability to maintain vibrancy throughout its lifecycle.
Colour Masterbatches for Diverse Industry Applications.
Our colour masterbatches serve a huge segment of the market, particularly in the woven sack, injection moulding and houseware segments.
Here, we provide solutions that offer excellent dispersion, uniformity and strength, helping our clients achieve significant cost efficiency without compromising on aesthetics.
Performance in PE Applications.
In PE applications, which dominate the flexible packaging and agricultural films sectors, we ensure high gloss, smooth finish and stability, even in challenging environmental conditions.
Our formulations are designed to support consistent colour performance while meeting the processing requirements of different plastic manufacturing applications.
Regulatory Compliance, Quality and Manufacturing Excellence.
We take regulatory compliance very seriously. Many of our masterbatches are approved for food contact applications, conforming to applicable national and international standards.
Our commitment to safety and sustainability drives us to continuously improve and innovate. We also offer non-heavy metal formulations, keeping in line with global eco-conscious trends.
World-Class Manufacturing Infrastructure.
We have world-class manufacturing infrastructure, strategically located across regions, equipped with cutting-edge technology and led by teams of highly skilled technicians and engineers.
Stringent Quality Checks at Every Stage.
Every batch we produce undergoes stringent quality checks, ensuring that what leaves our facility meets and exceeds expectations.
Our focus on precision, reliability and consistency enables customers to achieve dependable results across various applications.
A Partnership Beyond Colour Masterbatches.
Our technical and marketing teams work in sync with brand owners, converters and designers to understand their vision and translate it into material performance.
We believe in offering not just a product, but a partnership—one that begins at the concept stage and continues through manufacturing and post-production support.
Adapting to Changing Colour and Design Trends.
We also know that trends change. Colour preferences shift with seasons, industries and consumer moods.
Hence, we adapt smoothly to client recommendations aligned with current and emerging design trends, while maintaining the quality and consistency expected from our formulations.
Sustainability as a Core Principle.
Sustainability is another pillar of our brand's core principles. We are deeply aware of the responsibility that comes with operating in our industry.
Hence, we offer eco-friendly alternatives and work constantly towards reducing our environmental footprint through responsible material choices and continuous improvements in our processes.
Plastiblends: Bringing Colour Masterbatches to Global Markets.
Today, we export to over 60 countries across the globe, and our colour masterbatches are trusted by leading brands.
Our international presence is a testament to our consistent quality, technical support and commitment to innovation.
Looking ahead, we remain focused on pioneering new technologies that respond to evolving market demands. From heat-stable and UV-resistant formulations to smart tools, we aim to redefine the sector of masterbatches.
Frequently Asked Questions (FAQs)
1. What are colour masterbatches used for?
Colour masterbatches are used to add consistent, vibrant and long-lasting colour to plastic products during manufacturing. They are widely used in packaging, automotive, agriculture, electronics, injection moulding and houseware applications.
2. What are the advantages of colour masterbatches over powder pigments?
Colour masterbatches offer better pigment dispersion, reduced dust, improved processing cleanliness and precise colour control compared to traditional powder pigments. They also help manufacturers achieve greater consistency in finished plastic products.
3. Does Plastiblends offer customised colour masterbatches?
Yes. Plastiblends offers over 2,500 existing colour shades and has in-house colour matching laboratories that work with customers to develop customised formulations based on their specific application and performance requirements.
4. How do colour masterbatches improve plastic product performance?
Depending on their formulation, colour masterbatches can provide high opacity, excellent colour consistency, UV stability and resistance to weathering. These properties help plastic products maintain their appearance and performance throughout their intended lifecycle.
5. Are Plastiblends Colour Masterbatches suitable for food contact applications?
Many Plastiblends masterbatches are approved for food contact applications and conform to applicable national and international standards. Suitability depends on the specific formulation, intended application and relevant regulatory requirements.
6. Why choose Plastiblends as a colour masterbatches manufacturer?
Plastiblends combines advanced pigment dispersion technology, over 2,500 colour shades, customised formulations, stringent quality checks and technical expertise. With exports to over 60 countries, the company provides colour masterbatch solutions for diverse industrial applications.
- How Plastiblends Brings Colour Masterbatches to Life
- Masterbatches: The Backbone of Plastics
- How Masterbatches are Transforming the Indian Plastic Industry
- White and Black Masterbatches Define More Than Colour
- How Flexible Plastic Packaging Is Redefining Consumer Convenience
- The Role of Black Masterbatch Manufacturers in Modern Plastics
- The Role of Filler Masterbatches in Effective Cost Control and Beyond
- Why White Masterbatch Manufacturers Are Key to Packaging and Product Aesthetics
- Inside the World of Flexible Plastic Packaging – Trends and Technologies
- The Role of Carbon Black Masterbatch in Modern Plastics
- From Automotive to Agriculture: Why Black Masterbatch Remains in Demand
- 5 Trends Transforming the Rigid Plastic Packaging Industry in the Long Term
- How Automotive Plastic Additives are Revolutionising Car Components
- Inside a Masterbatches Manufacturer’s Lab: The Science of Colour and Performance
- The PET Masterbatch Advantage in Modern Packaging
- The Rise of PP Masterbatch and How It’s Transforming Modern Manufacturing
- A Deep Dive into Carbon Black Masterbatch: Science, Applications & Innovation
- Inside the World of White Masterbatch Manufacturers
- The Real Reason Flexible Plastic Packaging Continues to Outpace Other Formats
- How Plastic Masterbatches Enable Consistency in an Inconsistent Market
- Thermoplastic Compounds and the New Definition of Material Flexibility
- Plastic Compounds and the End of Single-Property Plastics
- Additive Masterbatch Innovations Transforming Thermoplastic Compounds and Cable Insulation
- Flexible Plastic Packaging Explained: How Plastic Compounds and Masterbatches Drive Performance
- Inside Pharmaceutical Packaging: Why Additive Masterbatch and Colour Masterbatch Are Non-Negotiable
- The Science of Strength: Carbon Black Masterbatch, Conductive Masterbatch and Advanced Plastic Compounds
- Inside the Growth of Filler Masterbatches: Where Cost Efficiency Meets Performance in Plastic Compounds
- The Evolution of Plastic Masterbatch Manufacturers in India: From Commodity to Innovation Leaders
- Thermoplastic Compounds: The Backbone of Next-Gen Plastic Masterbatch Manufacturing
- White Masterbatches and the Science of Premium Aesthetics in Plastic Products
- From Concept to Component - How Engineering Compounds Are Redefining Material Performance Across Industries
- Invisible Protection - How Antioxidant Masterbatch Extends the Life of Plastics in High-Temperature Applications
- The Shift Toward Lightweighting: A Competitive Edge for Rigid Plastic Packaging Manufacturers
- What Automotive OEMs Look for in Black Masterbatch Manufacturers in 2026
- Colour Masterbatches Are Becoming a Design Language in Manufacturing
- Engineering Compounds: The Backbone of Modern Plastic Applications
- How Smart Compounding is Shaping Everyday Products
- Why the Automotive Industry Relies on Specialised Plastic Compounds Today
- Conductive Compounds in Automotive Electronics: Meeting the Demands of EV Components
- How Rigid Plastic Packaging Manufacturers Are Adapting to India's New Recycled Content Regulations
- How to Choose the Right PP Masterbatch for Packaging, Automotive, and Textile Industries
- What Are Thermoplastic Compounds and Why Do They Matter?
- Automotive Compounds: What Makes Modern Vehicles Lighter, Safer and More Durable
- Beyond Colour: How Masterbatch Producers Are Driving Material Performance
- Heat, Processing and Performance: Why Antioxidant Masterbatch Is Essential
- How Flexible Plastic Packaging Manufacturers Improve Products' Shelf Life